China Best Wire to Board Connector Suppliers?
Choosing reliable China best wire to board connector suppliers requires more than comparing catalog prices. A suitable supplier must understand current, signal, power, and compact PCB applications. It should also provide clear drawings, stable materials, and repeatable production controls. In practical evaluations, buyers often inspect terminal plating, housing temperature ratings, contact retention, and mating cycles. Small details matter. A loose crimp can interrupt an entire control panel.
Experienced suppliers usually support custom pitch, locking structures, cable lengths, and surface treatments. However, customization should not become a substitute for engineering discipline. Ask for dimensional reports, material certificates, sample testing, and evidence of quality management. Factory audits, production photographs, and traceable batch records can strengthen confidence. Independent testing may still be necessary for demanding automotive, industrial, or medical applications. No supplier is perfect.
This guide examines how to compare Chinese manufacturers through product capability, technical communication, quality consistency, and delivery performance. It considers whether a supplier can move from a clear prototype to stable mass production without hiding limitations. Lead time claims deserve careful checking, especially during capacity changes or component shortages. A low quotation may reflect a simpler alloy, thinner plating, or weaker inspection process. That possibility should be tested, not assumed. We will also consider export experience, documentation accuracy, packaging protection, and after-sales responsiveness. The strongest choice is rarely the cheapest one. It is the supplier that explains risks honestly, validates performance with evidence, and improves when problems appear.
Wire-to-Board Connectors: 2.54 mm Pitch, 3 A Current, and 125°C Ratings
For buyers comparing China’s best wire-to-board connector suppliers, 2.54 mm pitch remains a practical specification. It suits control boards, sensors, lighting modules, and compact industrial equipment. Grand View Research estimated the global electrical connectors market at approximately USD 84.3 billion in 2023. That scale reflects demand, but not consistent quality.
A 3 A rating needs careful interpretation. It depends on contact resistance, wire size, ambient temperature, and acceptable temperature rise. A connector rated for 3 A at room temperature may require derating inside a 125°C enclosure. IEC 60512 testing methods help evaluate current-carrying capacity, contact resistance, and mechanical durability. Ask suppliers for test conditions, not only catalogue numbers.
The 125°C rating usually describes the housing material or maximum operating temperature. It does not guarantee 3 A performance at 125°C. Look for flame-retardant materials, secure terminal retention, and stable crimp geometry. Wire entry should feel firm, with no exposed conductor strands. Thermal cycling data matters.
A small detail can fail production.
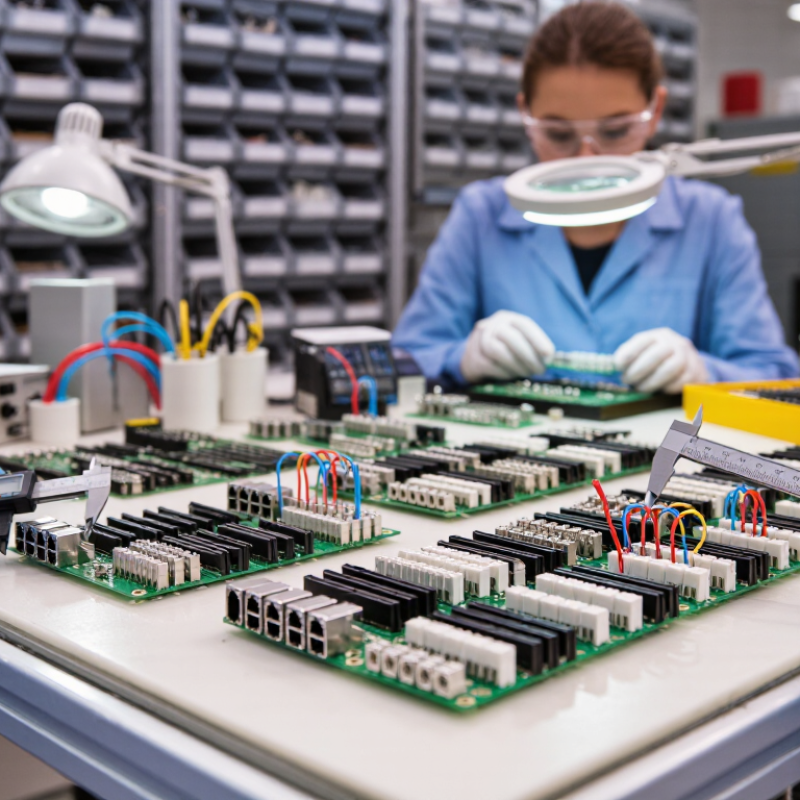
Supplier audits should include dimensional inspection, crimp pull-force records, and batch traceability. IPC industry reports continue to emphasize supply-chain resilience and documented process control across electronics manufacturing. Some datasheets remain vague, unfortunately. Confirm pitch tolerance, contact plating, mating cycles, and derating curves before sampling. A qualified supplier should provide samples, inspection records, and clear corrective-action procedures.
How to Evaluate Chinese Suppliers by ISO 9001, UL, RoHS, and IATF 16949
When evaluating Chinese wire to board connector suppliers, begin with documented quality systems, not polished catalogs. ISO 9001 should cover controlled drawings, inspection records, corrective actions, and employee training. Ask for the certificate’s scope, expiry date, and issuing body. A certificate alone proves little.
UL evidence should match the exact connector material, rating, and configuration. Check the file number and product markings against supplied samples. RoHS compliance requires current material declarations and, ideally, test reports for restricted substances. Do not accept a generic statement without component-level evidence. Small details matter.
For automotive applications, IATF 16949 indicates stronger process discipline, but it is not a guarantee of flawless production. Review control plans, process capability data, traceability, and change-management procedures. Request samples from normal production, not specially prepared units. Examine terminal retention, plating consistency, housing flash, and mating force. A supplier should explain failure handling with dates and responsible personnel. During an audit, compare paperwork with the factory floor. Sometimes records look perfect, while bins lack labels. That gap deserves attention. I have seen promising suppliers lose reliability after an unapproved material change, so written notification rules are essential. Ask how they manage subcontractors, tooling wear, and batch segregation. Leave room for doubt. It improves judgment.
Comparing Connector Types, Plating Options, and 30–500 Mating Cycles
When evaluating China-based wire-to-board connector suppliers, compare construction before comparing prices. Common options include crimp housings, pin headers, spring terminals, and insulation-displacement connectors. Crimp housings suit flexible cables and field assembly. Pin headers offer simple board mounting and predictable alignment. Spring terminals speed installation, but vibration can expose weak clamping designs. IDC connectors reduce stripping work, although cable tolerance becomes critical.
Plating often decides real contact life. Tin-plated contacts are cost-effective for low-cycle products and controlled environments. Their surfaces may oxidize after repeated handling. Nickel can provide a barrier layer, while gold plating usually supports lower resistance and higher durability. Ask for plating thickness, base material, contact resistance, and cross-section reports. A bright surface proves little. Small details matter. Cycle ratings should be read as test conditions, not promises. A 30-cycle connector may fit fixed equipment with rare servicing. A 100- to 200-cycle design suits removable modules and maintenance access. Heavy-use assemblies may require 300 to 500 cycles, especially with vibration or frequent inspection.
During supplier audits, request mating-cycle data, insertion-force curves, and post-test resistance readings. Test samples with the intended wire size and housing. Misalignment, side loading, dust, and excessive insertion speed can shorten service life. Still, ratings can mislead. Laboratory fixtures rarely reproduce every field condition. A reliable supplier should provide traceable samples, consistent molding records, and pilot-lot inspection data. I would also check terminal retention after repeated pulling, because this detail is easy to overlook.
China Best Wire-to-Board Connector Suppliers? Comparing Connector Types, Plating Options, and 30–500 Mating Cycles
Typical rated mating-cycle ranges for common wire-to-board connector formats. Gold-plated contacts generally support more mating cycles than tin-plated contacts, while the actual rating depends on contact design, insertion force, environment, and applicable product specifications.
Reference values shown: tin-plated contacts are commonly rated around 30 cycles, while gold-plated contacts are often specified from approximately 100 to 500 cycles for repeated-connect applications.
China’s Leading Supplier Categories for Automotive, Industrial, and Consumer Electronics
China Best Wire to Board Connector Suppliers?
China’s wire to board connector suppliers serve three major markets: automotive, industrial equipment, and consumer electronics. Each category requires different contact systems, housings, and validation methods. Automotive suppliers usually focus on vibration resistance, temperature stability, and secure locking structures. Engineers may request crimp terminals rated for engine compartments or battery systems. Sample testing should include pull-force checks, mating cycles, and thermal aging.
Industrial connector suppliers often support control cabinets, sensors, robots, and power equipment. Their products need stable insulation, clear polarity marks, and reliable performance in dusty workshops. Ask for material specifications, dimensional drawings, and batch inspection records. Some factories offer custom pitch, cable length, and terminal plating options. However, attractive samples do not always prove consistent mass production.
Consumer electronics suppliers work with compact housings, fine pitches, and automated assembly requirements. Camera modules, displays, and smart devices may need low-profile connectors with precise tolerances. I once underestimated packaging quality during supplier evaluation. Several contacts arrived bent after transport. That mistake changed my inspection checklist. Now, I review tray design, moisture protection, production capacity, and traceability before approving a supplier. Independent laboratory reports can strengthen confidence, but factory communication still matters. Clear drawings and controlled revisions prevent small design changes from becoming expensive failures.